Discover our globally certified commercial and architectural luminaires
Two Decades of Engineering Excellence in Global Illumination
Haining Glow Light Co., Ltd. is a professional lighting manufacturer established in 2002, integrating design, research and development, production, and comprehensive after-sales service. With over two decades of industry experience, we are committed to delivering high-quality decorative and industrial lighting solutions to customers worldwide.
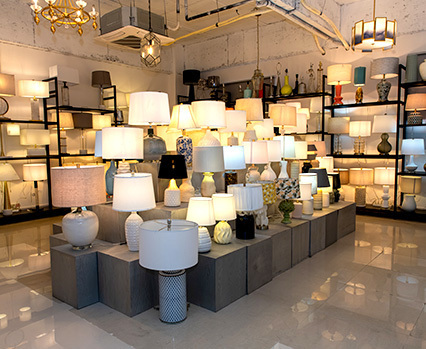
Our product range covers a wide variety of materials and styles, including Tiffany stained glass, vintage glass, wrought iron, hemp rope, marble, crystal, resin, shells, and other mixed-material designs. We specialize in decorative table lamps, floor lamps, wall lamps, pendant lamps, ceiling lamps, and robust outdoor illumination systems widely used in residential, commercial, and hospitality spaces.
Glow Light has built a strong and experienced R&D team with independent innovation capabilities. We support customized design and OEM/ODM services, enabling us to develop unique lighting products tailored to specific market demands and client requirements. From concept design to mass production, we ensure efficiency, creativity, and consistent quality.
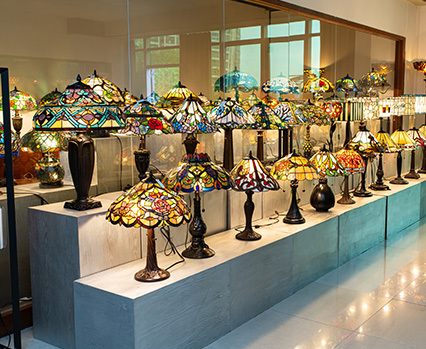
Our company has passed the SEDEX 4P factory audit, demonstrating our commitment to ethical business practices and responsible manufacturing. Our core team members each have over 10 years of experience in the lighting industry, ensuring professional management and product excellence.
All products comply with international standards and hold certifications such as UL, cUL, CE, RoHS, VDE, and GS. We also provide professional lighting testing reports and hold multiple design patents. These qualifications enable our products to meet the regulatory requirements of major global markets.
Our products are mainly exported to Europe and North America, serving major retailers, wholesalers, and project clients. We have earned a strong reputation for reliable quality, competitive pricing, and excellent customer service.
Our Mission: We are dedicated to providing outstanding service, maintaining superior quality, and driving innovation. With quality as our foundation and customer satisfaction as our core, we strive to create long-term value for our partners.
We warmly welcome customers from all over the world to visit Haining Glow Light Co., Ltd. and explore opportunities for cooperation.
Next-Generation Innovations in High-Power LED Floodlighting
Transitioning from conventional aluminum fin extrusion to advanced graphene-infused heat sinks and vapor-chamber technologies. This breakthrough ensures junction temperatures remain below critical thresholds, elevating luminous efficacy maintenance ($L_{90} > 100,000\text{ hours}$) in extreme outdoor operational environments.
Embedding Zigbee, DALI-2, and LoRaWAN communication protocols directly into CE certified LED floodlight drivers. This facilitates real-time telemetry, adaptive dimming schedules, fault diagnostics, and seamless integration into smart city municipal grids.
Designing future-proof architectures featuring toolless driver replacement and modular LED light engines. Complying strictly with upcoming European Union Ecodesign regulations and right-to-repair directives, minimizing carbon footprints across product lifecycles.
Engineered for Harsh Environments and High-Stakes Applications
High-salinity marine environments demand robust anti-corrosion protection. Our floodlights utilize marine-grade die-cast aluminum housing treated with AkzoNobel powder coating and 316 stainless steel hardware, enduring salt spray tests exceeding 1,000 hours.
Precision optical beam shaping minimizes light spill and glare for professional broadcasting (HD/4K ultra-slow-motion cameras). Flicker-free drivers ensure optimal visual comfort for athletes and spectators alike.
Impact-resistant tempered glass and IK10 mechanical strength ratings protect against falling debris and intense vibration from heavy machinery, ensuring unbroken operational continuity.
Navigating International Standards with Uncompromising Rigor
Our manufacturing facilities and products undergo rigorous testing by recognized independent laboratories (TÜV, SGS, Intertek). Full compliance packages including CE, RoHS, LVD, EMC, and CB reports are readily available for immediate customs clearance and project bidding.
Tailoring input voltage configurations from universal multi-voltage drivers (100-277V AC) to industrial high-voltage variations (347-480V AC), paired with robust 10kV to 20kV surge protection devices to withstand lightning strikes and grid fluctuations.
Offering comprehensive Dialux simulation services, photometric data files (IES/LDT), and customized OEM/ODM structural design support to ensure flawless project execution from blueprint to final installation.
Advanced Manufacturing Infrastructure and Quality Control Excellence
Equipped with high-speed Yamaha SMT placement machines, automated optical inspection (AOI) systems, and robotic soldering stations. This minimizes human error and guarantees exceptional PCB assembly consistency.
Every single floodlight undergoes a rigorous 48-hour high-temperature aging test, waterproof IP68 immersion testing, and integrating sphere photometric verification before packaging, ensuring a defect rate of less than 0.1%.
Strategically positioned near major shipping ports with streamlined ERP inventory management, guaranteeing agile lead times and secure, damage-resistant export packaging for international freight.
What B2B Buyers Look for in Certified LED Floodlight Partners
Global distributors and EPC contractors require manufacturing partners capable of scaling production rapidly while maintaining strict branding, custom casing, and proprietary driver specifications.
Enterprise clients demand 5-year to 7-year comprehensive warranties backed by audited financial stability and proven field performance records across municipal and commercial installations.
Corporate social responsibility (CSR) mandates require verified factory audits like SEDEX 4P, ensuring fair labor practices, safe working conditions, and environmentally responsible manufacturing processes.
Expert Insights on LED Flood Light Sourcing and Specifications
For the European market, CE, RoHS, and LVD/EMC compliance reports are mandatory, alongside ENEC marks for premium quality assurance. For North America, UL or cUL certification is required to meet local electrical safety codes and insurance regulations.
We utilize high-conductivity die-cast aluminum housings combined with finned heat sink geometry and optimal thermal interface materials (TIM). This ensures rapid heat dissipation, preventing lumen depreciation and driver failure over prolonged operation.
Yes. With over two decades of manufacturing experience, we offer complete OEM/ODM services—including custom laser-etched branding, bespoke color housing finishes, specialized driver integration, and professional Dialux IES photometric simulations for commercial projects.
Complete your project requirements with our extensive catalog
 Glow Light